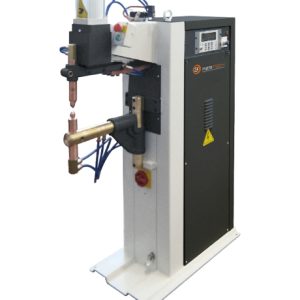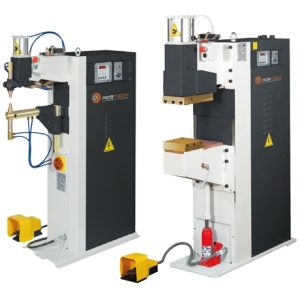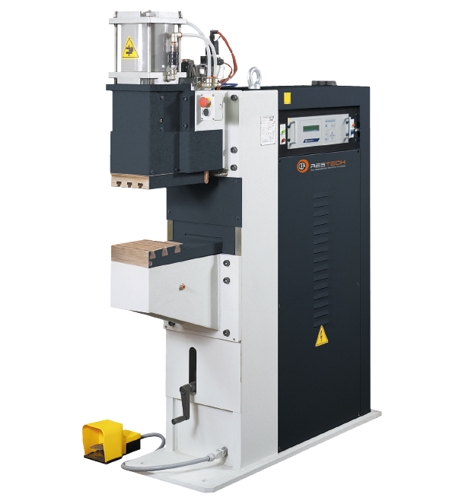
PPS range suitable for spotwelding only, whilst PPN machines are more versatile.
A large variety of MF series, i.e. Medium Frequency versions in DC plus PPN3FCC, DC conventional.
BSW bench welders complete this family.
| TECHNICAL DATA | MF 100 | MF 160 | MF 200 | |
|---|---|---|---|---|
| Single phase input50/60 Hz | V | 460 | 460 | 460 |
| Rated power at 50% | kVA | 100 | 160 | 200 |
| Installed power | kVA | 50 | 70 | 100 |
| Cross section connecting cables | mm2 | 35 | 50 | 70 |
| Fuse(delayed action) | A | 63 | 100 | 160 |
| Secondary voltage – OCV | V | 10 | 10 | 12 |
| Secondary short circuit current | kA | 28 | 45 | 55 |
| Max welding current ED 5% | kA | 20 | 36 | 36 |
| Secondary thermic current – ED 100% | kA | 6,5 | 12 | 12 |
| Work stroke | mm | 75 | 100 | 100 |
| Electrode force at 600kPa (6bar) | da N | 900 | 1200 | 1800 |
| Water consumption at 300kPa(3bar) | l/min | 20 | 20 | 20 |
| Dimensions |  mm |
1115 | 1115 | 1210 |
 mm |
400 | 400 | 460 | |
 mm |
1650 | 1650 | 1800 | |
| Weight | kg | 530 | 550 | 850 |